FDA Approval of Tecentriq for Stage III dMMR Colon Cancer and Pharma Supply Chain Impacts
The United States Food and Drug Administration recently approved the first adjuvant immunotherapy regimen for stage III mismatch repair deficient colon cancer. This landmark decision integrates Tecentriq with standard fluoropyrimidine and oxaliplatin chemotherapy. Clinical data from the ATOMIC trial demonstrates that this combination cuts the risk of recurrence or death by 50 percent. This breakthrough fundamentally alters the global oncology manufacturing landscape. Pharmaceutical procurement teams must now prepare for increased demand in specialized biologic and cytotoxic raw materials. The integration of immunotherapy into standard adjuvant care requires precise supply chain coordination. Manufacturers must secure high-purity chemical intermediates to support this new standard of care. Sourcing strategies must adapt to the complex formulation requirements of combined oncology regimens.
Clinical Impact of the ATOMIC Trial Data
The ATOMIC trial established a new benchmark for adjuvant colon cancer treatment. Patients receiving the combination therapy experienced a dramatic 50 percent reduction in recurrence or death risk. This statistical significance validates the synergistic effect of immune checkpoint inhibition and traditional chemotherapy.
Mismatch repair deficient tumors respond uniquely to immunotherapy agents. The addition of Tecentriq amplifies the immune system response against residual cancer cells. Clinicians will rapidly adopt this regimen for eligible stage III patients.
This clinical success drives immediate commercial scaling requirements. Pharmaceutical companies must accelerate their manufacturing timelines to meet projected patient demand. Procurement professionals must align their sourcing strategies with these aggressive production schedules.
Manufacturing Demands for Combined Oncology Regimens
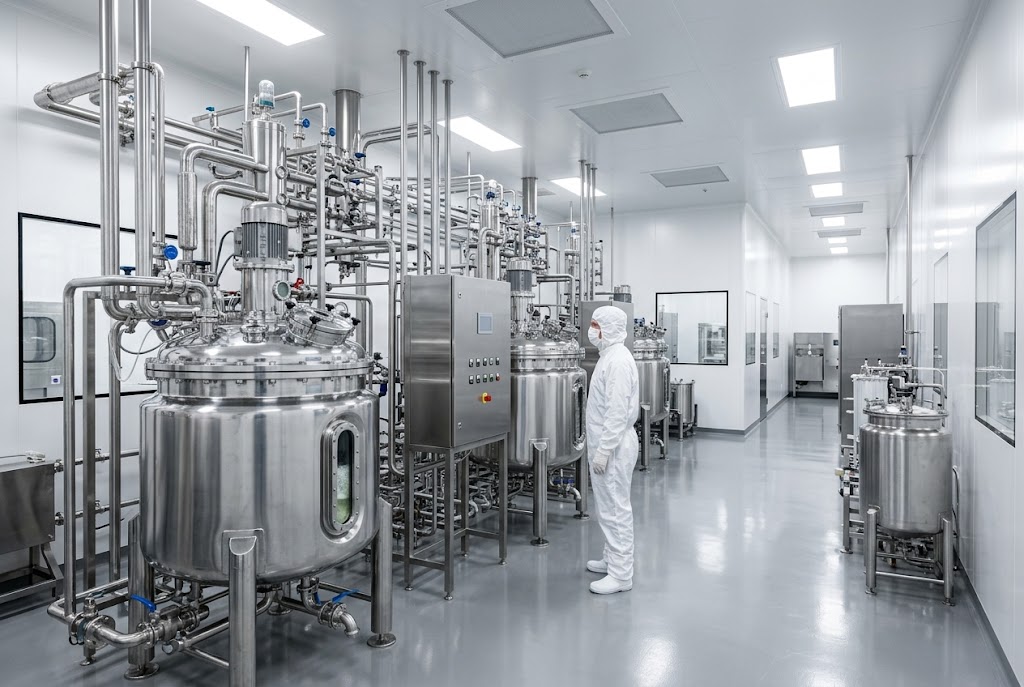
Producing combined oncology therapies requires highly specialized manufacturing infrastructure. Facilities must maintain strict adherence to current Good Manufacturing Practices at all times. The production process relies on a steady supply of high-purity raw materials and specialized excipients.
Buffering agents and stabilizers play a vital role in maintaining drug integrity. Sourcing these components from reliable global suppliers remains absolutely essential. Manufacturers cannot compromise on the quality of these foundational chemical ingredients.
Sterile filling operations demand precise environmental controls and advanced monitoring systems. Contamination risks must be minimized at every stage of the manufacturing process. This requires advanced facility design and rigorous daily operational protocols.
Scaling up production for both biologic and cytotoxic components presents unique engineering challenges. Facilities must isolate production lines to prevent cross-contamination. Dedicated equipment and specialized HVAC systems are mandatory for these high-potency active pharmaceutical ingredients.
Key Raw Materials in Oncology Formulations
The formulation of advanced oncology drugs depends on a precise balance of active and inactive ingredients. Excipients ensure the drug remains stable during extended storage and clinical administration. Common requirements include high-purity buffering salts and specialized isotonicity agents.
Suppliers must provide these materials with strict adherence to established pharmacopeial standards. Any variation in particle size or chemical purity can alter the final product performance. Procurement teams must specify exact grade requirements in their formal purchasing contracts.
High-purity solvents are critical for synthesizing complex cytotoxic compounds safely.
Specialized buffering agents maintain the precise pH required for biologic stability.
Sterile water for injection serves as the foundational vehicle for these potent therapies.
Sourcing these materials requires rigorous vendor qualification processes. Buyers must evaluate supplier capacity, quality control systems and geographic stability. Long-term supply agreements help secure consistent pricing and guaranteed material allocation.
Pharmaceutical grade acids and bases are frequently required for pH adjustment during synthesis. Procurement specialists must verify the heavy metal limits and residual solvent profiles of these reagents. Strict documentation ensures full compliance with international regulatory standards.
Supply Chain Risks and Sourcing Challenges
The oncology supply chain faces unique vulnerabilities that procurement teams must actively manage. Geopolitical tensions and trade restrictions can disrupt the flow of critical raw materials. Single-source dependencies increase the risk of severe production delays.
Companies must diversify their supplier base to mitigate these operational vulnerabilities. Establishing secondary sourcing channels for key pharmaceutical ingredients ensures long-term resilience. Regular supply chain audits help identify potential bottlenecks before they escalate into crises.
Transportation logistics also present significant challenges for temperature-sensitive components. Cold chain integrity must be maintained from the raw material supplier to the final manufacturing site. Investing in robust logistics partnerships protects product quality and prevents financial losses.
Port congestion and freight capacity constraints can delay the arrival of bulk chemical shipments. Buyers should maintain strategic safety stock levels for critical raw materials. This buffer protects manufacturing schedules from external logistical shocks.
Currency fluctuations can further complicate international procurement operations. Procurement managers should utilize financial hedging strategies to manage exposure. Diversifying supplier locations across different economic zones provides an additional layer of financial protection.
Quality Assurance and Regulatory Compliance
Pharmaceutical manufacturers must enforce rigorous quality assurance protocols at every stage of production. Regulatory agencies demand complete traceability for all raw materials and chemical intermediates. Suppliers must provide comprehensive certificates of analysis and adhere to international quality standards.
Any deviation in raw material quality can compromise the entire oncology batch. Procurement professionals must prioritize suppliers with proven compliance records and transparent auditing processes. Building trust with suppliers facilitates smoother regulatory inspections and faster batch releases.
Continuous monitoring of supplier performance is a non-negotiable industry requirement. Quality agreements should clearly define expectations and corrective action procedures. This proactive approach prevents costly batch rejections and unexpected production halts.
Auditing supplier facilities provides direct visibility into their operational capabilities. Procurement teams should request recent audit reports and corrective action plans. This diligence ensures alignment with internal quality management systems.
Regulatory bodies frequently update their guidelines for biologic and cytotoxic manufacturing. Procurement teams must stay informed about these evolving compliance standards. Adapting quickly to new regulations prevents costly operational disruptions and maintains market access.
Market Outlook for Adjuvant Immunotherapy
The successful progression of this regimen highlights the growing demand for targeted oncology therapies. Mismatch repair deficient colon cancer represents a significant clinical focus globally. As new treatments reach the market, competition will drive innovation in drug delivery and formulation.
Manufacturers will seek more efficient production methods to reduce overall operational costs. This dynamic environment creates opportunities for agile suppliers who can meet evolving technical specifications. Chemical traders who understand these specific pharmaceutical needs will capture greater market share.
The broader healthcare sector continues to prioritize innovative biologic treatments. Investment in research and development will only accelerate this industry trend. Supply chain partners must scale their capabilities to match this sustained market growth.
Emerging markets will increasingly demand access to these advanced therapies. This global expansion will further strain existing raw material supply networks. Proactive capacity planning is essential for all stakeholders in the pharmaceutical value chain.
What Procurement Teams Need to Know
Procurement leaders must proactively adapt their strategies to support the next wave of oncology biologics. Building strong relationships with qualified chemical and excipient suppliers is paramount. Teams should conduct regular risk assessments on their current supply networks.
Investing in supplier development programs can yield long-term stability and cost advantages. Early preparation ensures uninterrupted access to critical manufacturing inputs. Cross-functional collaboration between procurement, quality assurance and regulatory affairs is essential.
Aligned teams can respond faster to supply chain disruptions. This unity drives overall operational excellence in modern pharmaceutical manufacturing. Ready to source Glacial Acetic Acid from verified global suppliers? Explore competitive offers on our platform today.
Source:
https://chemxplore.com/news/fda-approves-tecentriq-dmmr-colon-cancer
Glacial Acetic Acid (99.8%) - China
Found this useful?