Casale’s Nitric Acid Plant for BorsodChem Starts Up on Schedule
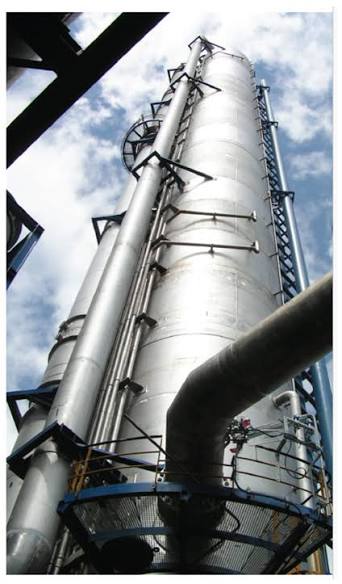
Casale’s successful start-up of a 450 metric tonnes per day (MTD) nitric acid plant for BorsodChem marks an important milestone for European chemical manufacturing. The facility produced its first nitric acid on 30 September 2026, following a start-up sequence that took approximately 12 hours.
The project has also moved quickly into operational activity. Production has reached approximately 1,000 tonnes and the plant has started exporting steam, demonstrating how modern chemical facilities can support both material production and wider site energy requirements.
For chemical traders, procurement managers and industrial buyers, this development highlights the relationship between production capacity, reliable feedstock availability and integrated manufacturing operations. It also provides a useful example of how new process technology can strengthen supply arrangements for downstream chemical producers.
Casale and BorsodChem Complete a Major Nitric Acid Project
The new plant operates at BorsodChem MCHZ's facility in Ostrava, Czech Republic. Casale received the project contract in 2024 and delivered it under a turnkey engineering, procurement and construction (EPC) arrangement.
The project brought together process engineering, equipment procurement, construction and commissioning within a coordinated delivery programme. Its on-schedule start-up demonstrates the importance of managing each stage carefully when bringing a complex chemical production unit into operation.
The facility uses Casale's proprietary DualPURE technology, which applies a dual-pressure process to nitric acid manufacturing. This approach targets efficient production, reliable operation and energy recovery, all of which matter to manufacturers seeking to control operating costs.
The plant's 450 MTD capacity gives BorsodChem an additional source of weak nitric acid for its industrial operations. Rather than treating the project simply as a new production line, buyers should view it as part of a wider effort to strengthen the integration between chemical manufacturing units.
Why Nitric Acid Matters to Industrial Supply Chains
Nitric acid is an essential inorganic chemical used across several industrial sectors. Its role in manufacturing makes dependable production important for companies that rely on consistent chemical inputs.
Key applications include:
Fertilizers: Nitric acid supports the production of nitrate-based fertilizers, which supply nitrogen to agricultural crops. Fertilizer manufacturers depend on reliable acid availability to maintain production schedules.
Chemical intermediates: Manufacturers use nitric acid in processes that produce compounds for further industrial conversion. These downstream materials serve a range of manufacturing markets.
Explosives: Industrial explosives producers use nitric acid in the manufacture of certain energetic compounds. This application requires strict process controls and compliance with applicable regulations.
Metals and surface treatment: Nitric acid supports selected metal processing, cleaning and treatment operations, where chemical purity and controlled handling influence performance.
Specialty and industrial chemicals: Various chemical processes use nitric acid as a reagent or intermediate, making supply reliability important for production planning.
For procurement teams, the breadth of these applications explains why a plant start-up can matter beyond the immediate manufacturer. Additional dependable capacity can support downstream production, although its effect on regional availability depends on actual output, internal consumption and existing supplier commitments.
DualPURE Technology and the Importance of Energy Recovery
Casale's DualPURE process forms the technical foundation of the new facility. The technology uses a dual-pressure configuration designed to combine production efficiency with energy recovery and operational reliability.
One notable feature is its ability to recover process heat and make steam available for export. This gives the facility an energy integration function alongside its primary role as a nitric acid producer.
The start of steam exports represents an important early operating milestone. It indicates that the plant has begun contributing to the site's broader utility network rather than serving only as an isolated production unit.
Energy recovery can influence several aspects of plant economics:
Utility efficiency: Recovering useful energy from the production process can reduce the need for separately generated steam, depending on site demand and system integration.
Operating expenditure: Efficient use of energy can help manufacturers manage a major component of industrial production costs.
Resource utilisation: Integrating recovered steam into other operations can improve the overall use of energy within a chemical complex.
Operational planning: Coordinating production with utility demand can help operators manage energy flows across interconnected manufacturing units.
These benefits depend on operating conditions, equipment performance and the site's ability to use recovered steam. The plant's continued ramp-up will therefore remain important as BorsodChem works towards stable, full-capacity operation.
What the 450 MTD Capacity Means for Production Planning
A nameplate capacity of 450 metric tonnes per day provides a useful reference point for understanding the scale of the installation. At continuous operation and full rated output, this capacity would correspond to approximately 164,250 tonnes per year, calculated over 365 days.
However, nameplate capacity does not represent guaranteed annual production. Maintenance, operating rates, feedstock availability, commissioning adjustments and unexpected interruptions can all affect the volume a plant actually delivers.
The reported production of approximately 1,000 tonnes shows that the facility has moved beyond initial start-up into active operation. The next stage involves stabilising the process and progressively increasing output towards its intended operating level.
For procurement managers, this distinction matters when assessing supply availability. A plant's announced capacity should not automatically translate into an assumption that the same quantity is immediately available for external sale.
BorsodChem can use the additional capacity to support its own downstream requirements. As a result, the plant's contribution to the open market may differ substantially from its total production capacity.
Buyers should monitor several indicators as operations mature:
Actual monthly production rather than nameplate capacity alone.
The proportion of output allocated to internal manufacturing requirements.
Maintenance schedules and expected operating rates.
Availability of ammonia and other essential inputs.
Contractual commitments that determine how much material remains available to third-party customers.
These indicators provide a more practical basis for procurement decisions than capacity announcements alone.
How the Start-Up Could Affect Chemical Buyers
The start-up gives BorsodChem a new production asset that can support its industrial operations. For buyers across the wider chemical supply chain, the most relevant question is how this additional capability may influence purchasing options, supplier reliability and regional trade flows.
The immediate impact will depend on the facility's operating performance and its role within BorsodChem's existing production network. If the plant primarily serves internal demand, its direct effect on merchant nitric acid availability may remain limited.
Nevertheless, stronger integration between production units can create indirect benefits. Reliable internal supply may help downstream manufacturers plan production more effectively and reduce their exposure to disruptions in external sourcing.
Procurement teams should consider the following implications:
1. Review regional supplier options. Buyers sourcing nitric acid or related chemical intermediates should track capacity developments across Central Europe and assess whether alternative suppliers can improve supply resilience.
2. Separate production capacity from merchant availability. A newly commissioned plant does not necessarily offer material for spot purchases. Procurement teams should confirm whether a producer sells to external customers before treating its capacity as a sourcing opportunity.
3. Reassess delivery arrangements. Chemical buyers should evaluate transport distance, delivery frequency, storage requirements and supplier lead times when comparing sourcing options.
4. Monitor production stabilisation. Early production figures provide useful evidence of progress, but stable output over a longer period offers a stronger basis for assessing supplier reliability.
5. Avoid relying on a single supply assumption. Maintaining qualified alternatives can protect buyers against production interruptions, logistical constraints and unexpected changes in market availability.
For importers and distributors, these steps can help distinguish genuine purchasing opportunities from developments that mainly benefit integrated producers.
Project Execution Offers Lessons for Chemical Manufacturers
The project also highlights the importance of coordinated execution in industrial plant development. Casale received the contract in 2024 and reached first production in September 2026, bringing engineering, construction and commissioning together under a defined schedule.
Turnkey EPC projects place substantial responsibility on the contractor to coordinate the delivery process. Equipment specifications, construction interfaces, process integration and commissioning activities must align before the facility can produce commercial output.
The approximately 12-hour start-up sequence represents a key milestone in this project. A short start-up period can reduce the time required to move from commissioning activities into production, although it does not replace the longer process of stabilising the plant and demonstrating sustained performance.
For manufacturers planning similar investments, several lessons stand out:
Define operating requirements early. Clear specifications for capacity, product quality, energy consumption and environmental performance help align the engineering design with business objectives.
Coordinate equipment and construction schedules. Delays in critical equipment or site preparation can affect the entire commissioning timeline.
Plan for downstream integration. New production units should match the material and utility requirements of the wider facility.
Measure performance beyond first production. Sustained output, product quality, energy efficiency and reliable operation provide a more complete picture of project success.
These considerations apply across commodity chemicals, fertilizer intermediates and other process-intensive industries.
What Buyers Should Watch as the Plant Ramps Up
The successful start-up establishes an important operational milestone, but the next phase will determine how consistently the facility performs. BorsodChem must progress through its planned stabilisation and ramp-up activities before the plant reaches full-capacity operation and completes its performance testing.
For chemical buyers, this creates several areas to monitor. Actual production volumes, operating reliability and the integration of recovered steam can help indicate how effectively the facility performs under normal conditions.
Market participants should also distinguish between the project's operational significance and its direct commercial effect. The new plant expands BorsodChem's production capabilities, but its influence on external nitric acid prices and availability will depend on regional supply and demand, internal consumption and commercial sales arrangements.
Procurement teams can respond by reviewing supplier contracts, maintaining alternative sourcing channels and tracking developments in regional production capacity. Buyers who combine market monitoring with clear specifications and realistic delivery planning will be better positioned to manage changes in supply conditions.
Casale's on-schedule start-up for BorsodChem demonstrates how new process technology, coordinated project execution and energy integration can support industrial chemical manufacturing. As the 450 MTD facility progresses towards stable operation, its longer-term value will depend on consistent production, efficient resource use and its contribution to BorsodChem's downstream requirements.
Ammonia Anhydrous
Found this useful?