Chemical Recycling: Opportunities and Challenges in Plastic Waste Management
Plastic waste is becoming an important source of alternative raw materials for the global chemical industry. Traditional mechanical recycling cannot process every plastic waste stream effectively, particularly when materials contain multiple polymers, additives, food residues or complex multilayer structures.
Chemical recycling offers another approach by breaking plastic polymers into smaller chemical components, monomers or hydrocarbon feedstocks that manufacturers can use in further production. These processes create opportunities to recover value from difficult-to-recycle plastics, support circular manufacturing and reduce reliance on virgin petrochemical feedstocks.
However, commercial adoption depends on processing costs, energy consumption, waste collection systems and the quality of recovered materials. Understanding these factors is essential for chemical manufacturers, plastic producers, traders and industrial buyers evaluating new recycling supply chains.
1. What Is Chemical Recycling and How Does It Work?
Chemical recycling refers to technologies that change the chemical structure of plastic waste to produce useful chemical substances or feedstocks. Unlike mechanical recycling, which mainly involves sorting, washing, shredding and remelting plastics, chemical recycling breaks down or transforms polymer structures.
The resulting materials can include:
Monomers: Basic chemical building blocks that manufacturers can use to produce new polymers.
Hydrocarbon oils: Liquid products that can undergo further upgrading into petrochemical feedstocks.
Synthesis gas: A mixture primarily containing hydrogen and carbon monoxide, which can support further chemical production.
Purified chemical intermediates: Recovered substances suitable for selected industrial applications.
Chemical recycling can process certain mixed, contaminated and multilayer plastic waste streams that create difficulties for conventional mechanical recycling.
It should complement mechanical recycling rather than replace it. Clean plastic waste that mechanical processes can recycle efficiently should generally remain within established material recycling systems.
Wedocs+1
2. Major Chemical Recycling Technologies Used in Plastic Waste Management
Different chemical recycling technologies produce different outputs and require specific feedstock characteristics. Manufacturers select a process according to the plastic type, contamination level, desired product and available processing infrastructure.
Pyrolysis
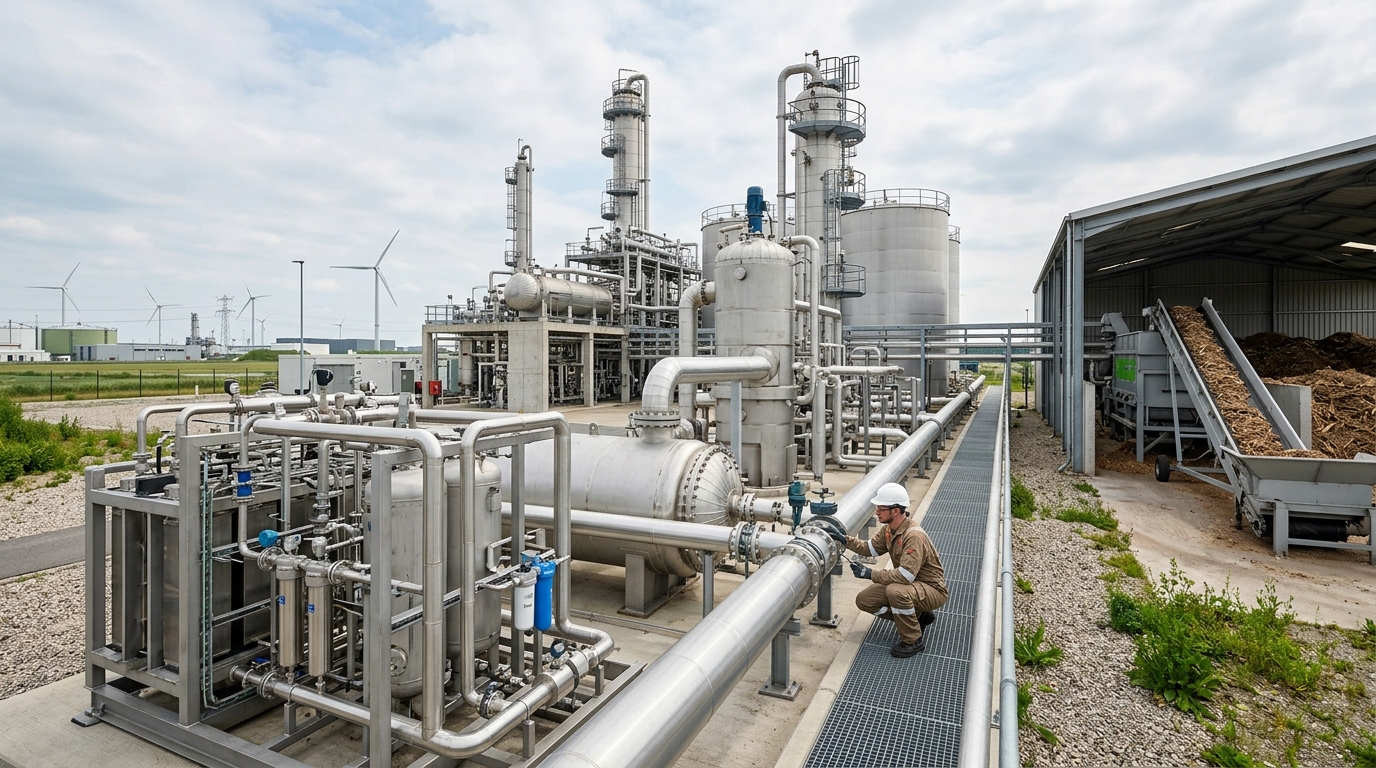
Pyrolysis uses high temperatures in an oxygen-limited environment to break down plastic waste into smaller hydrocarbons.
The process can produce:
Pyrolysis oil.
Hydrocarbon gases.
Solid carbon-rich residues.
The recovered oil may undergo additional purification and upgrading before entering petrochemical production. Suitable outputs can support the production of chemical feedstocks used in new plastics and other industrial products.
Polyethylene (PE) and polypropylene (PP) are among the plastic types commonly considered for pyrolysis.
Depolymerisation
Depolymerisation breaks polymer chains into their original monomers or other smaller chemical building blocks. It is particularly relevant to polymers with chemical structures that allow controlled breakdown.
For example, PET waste can undergo glycolysis, methanolysis or hydrolysis to recover chemical building blocks for further polymer production.
Recovered monomers require appropriate purification before manufacturers can use them in new polymer applications.
Gasification
Gasification converts carbon-containing waste into synthesis gas through high-temperature processing with a controlled amount of oxygen or steam.
The resulting hydrogen and carbon monoxide mixture can serve as a feedstock for producing methanol, hydrogen-based products and other chemicals, depending on the downstream processing system.
Solvolysis
Solvolysis uses solvents and controlled reaction conditions to break down selected polymers into reusable chemical components.
It has applications in recovering materials from PET, polyurethane and other suitable polymers. The process can produce valuable intermediates, although solvent recovery and purification influence its commercial performance.
Hydrothermal processing
Hydrothermal technologies use water under elevated temperature and pressure to transform selected plastic waste streams. Depending on the process, they can produce oils, gases or other chemical products.
Each technology has different operating requirements and material recovery potential. No single process can efficiently handle every type of plastic waste.
US EPA+2
3. Plastic Types Suitable for Chemical Recycling
Plastic composition plays a major role in determining which recycling technology can deliver useful outputs. Some polymers are suitable for recovering their original monomers, while others require thermochemical conversion.
Polyethylene Terephthalate (PET)
PET is widely used in beverage bottles, food packaging and synthetic fibres. Depolymerisation can recover chemical building blocks such as terephthalic acid and ethylene glycol, supporting the production of new PET materials.
High-Density Polyethylene (HDPE)
HDPE appears in detergent containers, industrial packaging, pipes and household products. Suitable HDPE waste can undergo pyrolysis to produce hydrocarbon feedstocks for further processing.
Low-Density Polyethylene (LDPE)
LDPE is common in flexible packaging, films and plastic bags. Its flexible structure and widespread use make it an important potential feedstock for thermochemical recycling.
Polypropylene (PP)
PP is used in automotive components, packaging, household products and industrial applications. Pyrolysis can convert suitable PP waste into hydrocarbon-rich products.
Polystyrene (PS)
Polystyrene is used in packaging, insulation and disposable products. Depolymerisation can recover styrene monomer from suitable waste streams, creating opportunities to manufacture new polystyrene.
The selection of plastic feedstock remains critical. Contamination, polymer mixtures, additives and degradation can affect conversion efficiency and recovered product quality.
4. Commercial Opportunities for Chemical Manufacturers and Buyers
Chemical recycling creates commercial opportunities across waste management, petrochemicals, polymer manufacturing and chemical distribution.
One important opportunity involves developing alternative feedstock supplies for petrochemical producers. Recovered oils, monomers and other chemical intermediates can supplement conventional raw materials when their specifications match industrial requirements.
Several market opportunities are emerging:
Recycled polymer production: Manufacturers can use suitable recovered monomers and feedstocks to produce new polymer materials.
Alternative petrochemical feedstocks: Recovered hydrocarbon oils can provide additional raw material options for selected chemical manufacturing processes.
Specialty chemical intermediates: Depolymerisation can recover chemical building blocks for producing polymers and other industrial compounds.
Recycling infrastructure investment: Demand for advanced sorting, purification and processing equipment creates opportunities for technology providers.
International feedstock trading: Recyclers and chemical manufacturers can develop supply agreements for suitable plastic waste and recovered chemical products.
Regulatory requirements for recycled content can also influence demand. The European Union's packaging and single-use plastics policies provide an important commercial context for manufacturers seeking recycled plastic inputs.
5. Environmental Benefits and Sustainability Considerations
Chemical recycling can contribute to plastic waste management by creating additional recovery options for materials that conventional recycling systems struggle to process.
Its potential environmental benefits include:
Reduced plastic disposal
Processing suitable plastic waste can divert materials from landfills and other disposal routes. This also creates opportunities to recover value from waste streams that would otherwise have limited recycling options.
Reduced demand for virgin feedstocks
Recovered monomers and hydrocarbon feedstocks can replace some conventional raw materials in new chemical production. The actual substitution depends on product quality and processing requirements.
Support for circular manufacturing
Chemical recycling can return selected plastic materials to chemical production systems rather than directing them towards disposal after a single use.
Improved material recovery options
Some chemical processes can handle contaminated or mixed plastic streams that mechanical recycling cannot process effectively.
However, environmental performance depends on energy consumption, process emissions, feedstock preparation and downstream product use. Life cycle assessment helps companies compare these factors against virgin production and alternative waste management methods.
Chemical recycling should therefore be evaluated according to its actual material recovery and environmental performance, not simply the amount of plastic entering a processing facility.
6. Key Challenges Affecting Chemical Recycling Investment
Despite its potential, chemical recycling faces several technical and economic barriers that influence investment decisions and commercial expansion.
High capital and operating costs
Chemical recycling facilities require specialised reactors, separation systems, purification equipment and supporting infrastructure. These investments can make recovered feedstocks more expensive than conventional petrochemical alternatives.
A 2026 European Commission Joint Research Centre assessment highlights that chemical recycling technologies still face economic challenges and have not achieved cost parity with virgin plastics in the EU.
High energy requirements
Processes such as pyrolysis and gasification require substantial heat and energy. Energy prices and the availability of lower-carbon electricity can therefore influence operating costs and environmental performance.
Feedstock contamination
Mixed polymers, food residues, dyes, additives and other contaminants can affect processing efficiency. Recycling facilities need reliable sorting and pretreatment systems to maintain consistent output quality.
Product purification requirements
Recovered oils and chemical intermediates may contain unwanted compounds. Additional upgrading and purification can increase costs before manufacturers can use these materials in production.
Limited commercial infrastructure
Many chemical recycling technologies still face challenges in scaling from pilot operations to consistent industrial production. Developing reliable waste collection networks and long-term feedstock contracts is equally important.
These challenges make technology selection, plant location and feedstock availability central considerations for investors.
7. Supply Chain, Quality Control and Regulatory Requirements
Chemical recycling connects waste management operations with conventional chemical manufacturing. This creates a supply chain that requires coordination between waste collectors, sorting facilities, recycling plants, chemical producers and downstream buyers.
For chemical traders and procurement managers, recovered feedstocks require the same commercial attention as conventional industrial materials.
Important purchasing considerations include:
Feedstock specifications: Confirm polymer composition, contamination levels, moisture content and material consistency.
Recovered product quality: Review chemical composition, purity, density and other relevant technical properties.
Supplier documentation: Request Certificates of Analysis (COA), Safety Data Sheets (SDS) and batch traceability records.
Regulatory compliance: Check applicable waste transportation, chemical registration and recycled-content requirements.
Supply reliability: Assess production capacity, delivery schedules and long-term availability.
Environmental credentials: Review lifecycle information and evidence supporting recycled-content or sustainability claims.
The ISO 15270 series provides guidance on plastics waste recovery and recycling, including principles relevant to chemical recycling.
For emerging markets, waste collection and sorting infrastructure also influence the commercial feasibility of recycling projects. A 2025 UNEP life cycle assessment examining plastic waste management technologies in Pakistan highlights the importance of evaluating collection, transportation, pretreatment and end-of-life processing together.
Wedocs
8. Market Outlook: The Future of Chemical Recycling
Chemical recycling is expected to remain an important area of development within the global plastics and petrochemical industries. Growing interest in recycled content, alternative feedstocks and circular manufacturing is encouraging investment in new processing technologies.
Several developments will influence future market growth:
Advanced pyrolysis systems: Improvements in reactor design and oil upgrading could improve feedstock quality and processing efficiency.
Depolymerisation innovation: Better recovery processes could expand the commercial recycling of PET, polyamides and other suitable polymers.
Petrochemical industry partnerships: Collaboration between recycling companies and polymer producers can connect recovered feedstocks with established manufacturing infrastructure.
Digital waste traceability: Better material identification and tracking can improve feedstock quality and supply chain transparency.
Recycled-content requirements: Regulatory developments can encourage manufacturers to incorporate suitable recycled materials into their products.
The industry will also need to improve energy efficiency, reduce processing costs and establish reliable markets for recovered outputs.
For chemical traders, these developments could create new opportunities in recycled polymers, recovered hydrocarbon feedstocks and chemical intermediates. Buyers who understand material specifications and supplier capabilities will be better positioned to participate in these emerging markets.
What Chemical Buyers Should Prioritise in Plastic Recycling Markets
Chemical recycling offers an additional route for converting plastic waste into commercially useful resources. Its ability to recover monomers, hydrocarbon feedstocks and other chemical intermediates creates opportunities for petrochemical producers and polymer manufacturers.
However, successful adoption depends on more than recycling technology. Feedstock quality, energy costs, purification requirements, regulatory compliance and reliable supply agreements all influence commercial viability.
Chemical manufacturers should evaluate recycling technologies according to their specific production requirements, while procurement teams should prioritise consistent specifications and qualified suppliers. Chemical traders can support this transition by connecting recycling facilities with industrial buyers seeking alternative raw materials.
As plastic waste management evolves, chemical recycling can become a valuable part of a broader circular plastics economy, complementing mechanical recycling and improving the utilisation of suitable waste materials.
Found this useful?