Chemical Catalysts: How They Improve Industrial Production Efficiency
Chemical catalysts help manufacturers increase production efficiency while controlling energy consumption, operating costs and material waste. From petroleum refining to fertilizer manufacturing, catalytic processes support some of the most important chemical transformations in modern industry.
A chemical catalyst accelerates a reaction without being consumed during the overall process. It can also help manufacturers achieve better product yields under less demanding temperature and pressure conditions, making production more economical and resource-efficient.
As industrial buyers face growing pressure to secure reliable supplies and manage production expenses, catalysts have become an important part of manufacturing strategy. Their performance influences production capacity, product quality and the long-term competitiveness of chemical processing operations.
What Are Chemical Catalysts and How Do They Work?
A chemical catalyst is a substance that increases the rate of a chemical reaction by providing an alternative reaction pathway with lower activation energy. Activation energy represents the minimum energy required for reactants to undergo a chemical transformation.
Without a suitable catalyst, certain reactions require substantial heat, pressure or extended processing time. A catalyst makes these reactions easier to initiate and maintain under controlled operating conditions.
Catalysts generally remain available for repeated reaction cycles, although industrial operating conditions can gradually reduce their activity. Manufacturers must therefore monitor catalyst performance and replace or regenerate materials when necessary.
Three important characteristics determine how effectively a catalyst supports industrial production:
Activity: Determines how quickly a catalyst converts reactants into products. Higher activity can help manufacturers achieve production targets with shorter reaction times or smaller reactor systems.
Selectivity: Determines how strongly a catalyst favours the desired chemical product over unwanted byproducts. Better selectivity reduces material losses and simplifies downstream purification.
Stability: Determines how well a catalyst maintains its performance under operating conditions. Stable catalysts support longer production campaigns and reduce replacement frequency.
These characteristics work together to determine the commercial value of a catalyst. A material that delivers high activity but loses performance quickly may prove less economical than a slightly slower catalyst with a longer operating life.
Major Types of Catalysts Used in Industrial Manufacturing
Different industrial reactions require different catalyst structures and chemical properties. Manufacturers select catalyst types according to the reaction mechanism, feedstock composition, operating environment and desired product.
The main categories include:
1. Homogeneous catalysts
Homogeneous catalysts operate in the same physical phase as the reactants, commonly within a liquid solution. They offer effective contact between reacting molecules and can provide high selectivity in chemical synthesis.
Industries use them in pharmaceutical manufacturing, fine chemicals and specialty chemical production. However, separating the catalyst from the final product can create additional processing requirements.
2. Heterogeneous catalysts
Heterogeneous catalysts exist in a different physical phase from the reactants. Solid catalysts used in liquid or gas-phase reactions are common examples.
These catalysts play a major role in petroleum refining, petrochemical production and large-scale chemical manufacturing. Their relatively straightforward separation and potential for regeneration make them suitable for continuous industrial operations.
3. Enzyme catalysts
Enzymes are biological catalysts that accelerate specific chemical reactions under relatively mild conditions. Their high selectivity makes them valuable in food processing, pharmaceuticals, biotechnology and certain specialty chemical applications.
4. Supported metal catalysts
These catalysts contain active metals distributed across a supporting material. Platinum, palladium, nickel and other metals can provide active reaction sites while the support helps distribute the catalytic material.
Their applications include hydrogenation, oxidation, reforming and emissions treatment.
Selecting the correct catalyst requires more than comparing reaction speed. Compatibility with feedstocks, operating temperatures, pressure requirements and product specifications also determines whether a catalyst can deliver consistent commercial performance.
How Catalysts Improve Industrial Production Efficiency
Catalysts influence several stages of industrial manufacturing, from raw material conversion to final product recovery. Their benefits extend beyond accelerating chemical reactions.
Lower energy consumption
Many industrial reactions require significant heat to overcome activation barriers. Catalysts reduce these barriers and can allow manufacturers to operate at lower temperatures or pressures.
This reduces the energy required for heating, compression and other supporting operations. Energy-efficient catalytic processes also help manufacturers control exposure to fluctuating electricity and fuel costs.
Department of Energy+1
Higher production rates
Catalysts can accelerate reaction rates, allowing manufacturers to process larger quantities of feedstock within a given period. Faster reactions can improve equipment utilization and increase overall plant throughput.
Improved product yield
A selective catalyst directs more reactants towards the desired product rather than unwanted secondary compounds. Manufacturers can therefore obtain more saleable output from the same quantity of raw materials.
Reduced waste and purification costs
Unwanted byproducts often require additional separation, treatment or disposal. Better catalytic selectivity can reduce these requirements and lower the resources needed to achieve final product specifications.
Better process economics
When manufacturers combine lower energy requirements, improved conversion rates and reduced material losses, they can strengthen overall production economics. These benefits can improve operating margins and make production facilities more competitive.
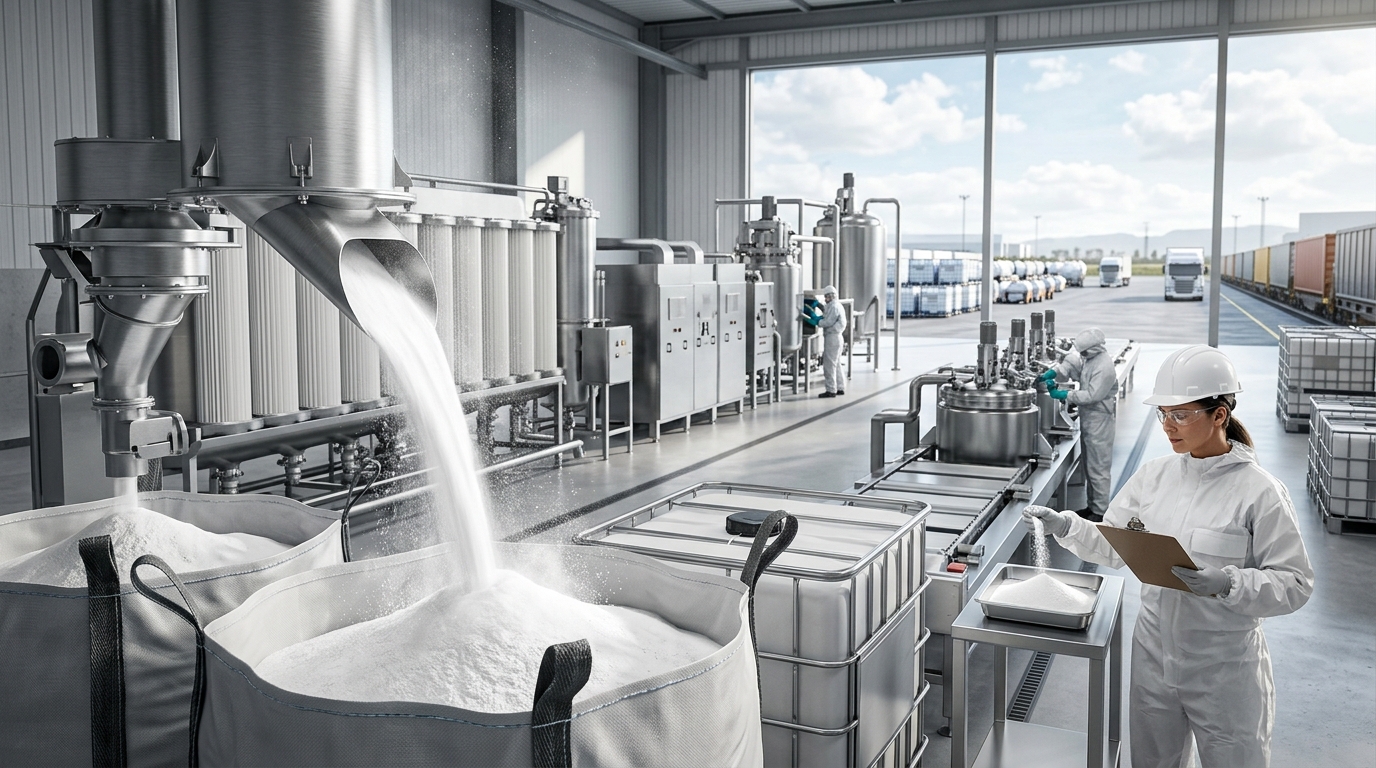
Industrial Applications Across Major Chemical Sectors
Catalysts support production processes across several industries. Their applications vary according to the chemical transformation required and the performance standards of the finished product.
Petroleum refining and petrochemicals
Refineries use catalysts in processes such as catalytic cracking, reforming and hydroprocessing. These operations help convert heavier petroleum fractions into more valuable fuels and chemical feedstocks.
Catalytic cracking supports the production of lighter hydrocarbons, while reforming helps generate high-octane gasoline components and important aromatic feedstocks. These processes also influence the availability of materials used in plastics, solvents and synthetic chemicals.
Fertilizer manufacturing
Ammonia production relies on catalytic technology through the Haber-Bosch process. Iron-based catalysts help nitrogen and hydrogen react to form ammonia under controlled industrial conditions.
Ammonia serves as a major feedstock for nitrogen fertilizers and several downstream chemical products. Efficient catalytic performance helps fertilizer manufacturers manage the substantial energy requirements associated with production.
Pharmaceuticals and fine chemicals
Catalysts enable precise chemical transformations during the manufacture of pharmaceutical ingredients and specialty compounds. Selective catalytic reactions can reduce unwanted impurities and support consistent product quality.
Manufacturers also use enzyme catalysts for reactions that require specific molecular structures or relatively mild processing conditions.
Polymer and plastics manufacturing
Catalysts influence polymerization reactions and help manufacturers control polymer structure, molecular weight and product characteristics. These properties affect the strength, flexibility and processing behaviour of finished plastics.
Catalytic technologies are particularly important in the production of polyethylene and polypropylene, two widely used industrial polymers.
Environmental and emissions treatment
Catalysts help convert harmful exhaust components into less harmful substances. Automotive catalytic converters, for example, support the treatment of carbon monoxide, hydrocarbons and nitrogen oxides.
Industrial facilities also use catalytic oxidation and other treatment processes to manage emissions and support environmental compliance.
Factors That Influence Catalyst Performance and Operating Costs
Even a well-designed catalyst may deliver inconsistent results when manufacturers overlook operating conditions. Several factors influence its activity, useful life and overall contribution to production efficiency.
Temperature and pressure: Every catalyst has an operating range. Excessive temperatures can damage its structure, while unsuitable pressure conditions can reduce reaction performance.
Feedstock quality: Impurities such as sulfur compounds, metals and other contaminants can occupy active sites or cause catalyst poisoning. Consistent feedstock quality helps maintain reliable reaction performance.
Catalyst particle size: Particle dimensions and surface characteristics influence contact between reactants and active catalytic sites. Poor particle distribution can affect conversion rates and reactor performance.
Deactivation and fouling: Carbon deposits, chemical contamination and thermal degradation can gradually reduce catalytic activity. These problems may increase energy requirements and force manufacturers to replace or regenerate catalysts.
Reactor design: Gas flow, liquid distribution and heat transfer affect how efficiently reactants interact with the catalyst. Suitable reactor design helps prevent uneven reaction conditions.
Catalyst deactivation deserves particular attention because it can create costs beyond the price of replacement material. Lower activity may reduce output, increase energy consumption and create additional separation requirements. The US Department of Energy highlights these challenges in its research on improving catalyst selectivity and longevity.
The Department of Energy's Energy.gov+1
Catalyst Sourcing, Quality Control and Supply Chain Considerations
For chemical buyers, catalyst procurement involves more than finding a competitive price. Product consistency, technical specifications and supplier reliability directly influence manufacturing performance.
A catalyst that differs from the required grade or composition can disrupt established production conditions. Procurement teams should therefore evaluate technical documentation alongside commercial terms.
Important sourcing considerations include:
Technical specifications: Buyers should confirm the catalyst's chemical composition, active metal content, particle size, surface area and physical form where relevant. These specifications should match the requirements of the intended process.
Purity and contamination limits: Manufacturers should review certificates of analysis and relevant impurity limits. Even small quantities of certain contaminants can affect catalyst activity or product quality.
Supplier consistency: Reliable suppliers should demonstrate the ability to maintain consistent product specifications across different shipments. This becomes particularly important for continuous manufacturing operations.
Packaging and transportation: Moisture-sensitive, temperature-sensitive or hazardous catalyst materials may require specialized packaging and handling. Buyers should confirm storage conditions, transportation requirements and applicable safety documentation before placing orders.
Supply availability and lead times: Some catalysts contain specialized metals or depend on concentrated raw material supply chains. Procurement teams should assess supplier capacity, alternative sourcing options and replenishment schedules.
A structured procurement strategy helps manufacturers reduce supply interruptions while maintaining control over production quality and operating expenses.
Sustainability and the Future of Catalytic Manufacturing
Industrial sustainability increasingly depends on improving how manufacturers use energy, raw materials and production equipment. Catalytic technologies can support these objectives by reducing reaction temperatures, improving conversion efficiency and limiting unwanted byproducts.
Green chemistry also encourages manufacturers to replace less efficient chemical pathways with selective catalytic alternatives. These approaches can reduce the need for additional reagents, minimize waste generation and improve the use of raw materials.
American Chemical Society+1
Several developments are shaping the next generation of catalytic manufacturing:
Advanced catalyst materials: Researchers are developing materials with improved activity, selectivity and resistance to deactivation. These improvements can extend operating life and reduce maintenance requirements.
Renewable feedstock conversion: Catalytic technologies can help transform biomass and other renewable resources into useful fuels, chemicals and industrial materials.
Carbon dioxide conversion: Researchers are exploring catalytic pathways that convert carbon dioxide into products such as methanol, formic acid and other valuable chemicals.
Digital process monitoring: Sensors, reaction modelling and process analytics can help manufacturers monitor catalyst behaviour and identify performance changes before they disrupt production.
Catalyst regeneration: Improved regeneration methods can restore the performance of certain spent catalysts, reduce replacement requirements and support more efficient material use.
The International Energy Agency's roadmap on catalytic processes identifies significant opportunities for reducing industrial energy consumption and greenhouse gas emissions through improvements in catalytic technology. These developments position catalysis as an important part of more resource-efficient chemical production.
IEA+1
What Procurement Teams Should Prioritize in the Coming Years
As manufacturers invest in production efficiency, procurement teams will play a larger role in selecting materials that support long-term operational performance.
The lowest purchase price does not always deliver the lowest production cost. A more expensive catalyst may offer better activity, longer service life or higher selectivity, ultimately reducing the total cost per unit of finished product.
Buyers should prioritize the following actions:
Evaluate total operating cost: Compare catalyst purchase prices with expected service life, regeneration requirements, energy consumption and production output.
Request technical documentation: Obtain certificates of analysis, safety data sheets and relevant product specifications before approving suppliers.
Assess long-term availability: Establish relationships with dependable suppliers and consider alternative sourcing arrangements for critical catalyst materials.
Monitor performance after procurement: Track conversion rates, product quality, catalyst consumption and replacement frequency to evaluate actual performance.
Consider sustainability requirements: Evaluate catalysts that support lower energy consumption, reduced waste generation and improved resource efficiency.
These measures help procurement professionals connect chemical sourcing decisions with wider manufacturing objectives. They also support better supplier negotiations and more predictable production planning.
The Bottom Line for Industrial Chemical Buyers
Chemical catalysts are essential to improving efficiency across modern industrial production. By accelerating reactions, enhancing selectivity and reducing energy requirements, they help manufacturers increase output while managing material consumption and operating expenses.
Their commercial value depends on choosing the right catalyst for each application and maintaining suitable operating conditions throughout its service life. For procurement teams, technical compatibility, consistent quality and dependable supplier relationships should remain central to every sourcing decision.
As catalytic technologies continue to advance, manufacturers will have greater opportunities to improve production performance and adopt more sustainable processing methods. Reliable chemical sourcing will remain an important part of that transition.
Ready to source Manganese Dioxide from verified global suppliers? Explore competitive offers on our platform today.
Sources:
Manganese Dioxide
Found this useful?