Industrial Catalyst Supports: Types, Uses and Selection
Fire safety remains a major priority across construction, manufacturing, infrastructure and industrial processing. Fire retardant coatings provide an additional layer of protection by slowing flame spread, reducing heat transfer or helping structural materials withstand high temperatures during a fire.
These coatings support fire protection strategies in commercial buildings, warehouses, factories, power facilities and transportation infrastructure. For chemical traders, procurement managers and industrial buyers, understanding coating technologies and product specifications helps identify suitable materials for different applications. Selecting the correct formulation also supports regulatory compliance, equipment protection and long-term operational reliability.
What Are Fire Retardant Coatings?
Fire retardant coatings are specialised protective materials that improve the fire performance of surfaces such as steel, concrete, wood and other construction materials. Manufacturers formulate them with fire-resistant chemicals, binders, pigments and functional additives to achieve specific protection characteristics.
Unlike conventional decorative paints, these coatings serve a technical purpose. They help delay ignition, reduce flame propagation or protect the underlying substrate from excessive heat.
How Fire Retardant Coatings Work
Different formulations use different mechanisms to control fire exposure. Some coatings create an insulating barrier while others release substances that interfere with combustion.
Common protection mechanisms include:
Intumescent action: The coating expands when exposed to high temperatures, forming a thick insulating char layer that slows heat transfer to the underlying surface.
Flame inhibition: Special chemical ingredients help interrupt combustion reactions and reduce flame propagation.
Heat insulation: Protective layers reduce the rate at which heat reaches structural materials.
Smoke and combustion control: Certain formulations help reduce smoke generation or limit the release of combustible gases, depending on their composition and tested performance.
The effectiveness of each mechanism depends on the coating formulation, application thickness, substrate and fire exposure conditions.
Main Types of Fire Retardant Coatings
Industrial buyers generally encounter several coating categories:
Intumescent coatings: These coatings expand under heat and create an insulating carbon layer. They are widely used to protect structural steel in buildings and industrial facilities.
Cementitious fireproof coatings: These products contain cement-based materials and lightweight aggregates. They provide thick protective layers for structural components.
Thin-film fire retardant coatings: These coatings offer a relatively smooth finish and suit applications where appearance and limited coating thickness matter.
Water-based fire retardant coatings: These formulations use water as the primary carrier and may offer lower solvent emissions compared with conventional solvent-based alternatives.
Solvent-based fire retardant coatings: These products use organic solvents and can provide specific adhesion, curing and environmental performance characteristics required for particular applications.
Buyers should distinguish between fire retardant coatings and fire-resistant coatings because their functions and testing requirements may differ.
Industrial Applications of Fire Retardant Coatings
Fire retardant coatings serve multiple industries where fire exposure could damage assets, interrupt production or threaten human safety. Their selection depends on the substrate, operating environment and required fire protection period.
Construction and Structural Steel
Structural steel loses strength when temperatures rise significantly. Intumescent coatings help delay this temperature increase by expanding into an insulating layer when exposed to fire.
Construction companies use these coatings on:
Structural steel beams and columns.
Commercial buildings and office complexes.
Shopping centres and industrial warehouses.
Airports, railway stations and public infrastructure.
Steel frameworks in manufacturing facilities.
The required coating thickness depends on the steel section, its exposure conditions and the specified fire-resistance rating.
Oil, Gas and Petrochemical Facilities
Oil refineries, chemical plants and gas processing facilities handle flammable materials and operate equipment that requires specialised fire protection.
Fire protective coatings can support protection strategies for structural steel, processing facilities, storage areas and selected industrial equipment. Buyers must consider chemical exposure, moisture, temperature changes and corrosion risks when choosing coating systems.
Manufacturing and Industrial Warehousing
Manufacturing plants contain machinery, electrical installations, storage systems and structural components that may face fire hazards.
Fire retardant coatings can help protect building materials and selected equipment surfaces. In warehouses, coating selection should account for the stored materials, ventilation conditions and potential fire exposure.
Transport and Infrastructure
Railway facilities, tunnels, bridges and transportation buildings may also require fire protection systems. Specialised coatings can help protect structural components and selected interior surfaces.
Their performance must match the specific requirements of the infrastructure project, including environmental exposure, maintenance access and applicable safety standards.
Key Product Requirements for Fire Retardant Coatings
Product quality directly affects coating performance, durability and suitability for industrial use. Procurement teams should evaluate technical specifications rather than selecting products based only on price or general fire-retardant claims.
Fire Resistance Rating
The fire resistance rating indicates how long a tested assembly can maintain its required performance under specified fire exposure conditions.
Common project requirements include 30, 60, 90 and 120 minutes of fire protection. However, the appropriate rating depends on building regulations, structural design and project specifications.
Buyers should request test reports and certification documents that match the intended substrate and application.
Coating Thickness and Coverage
Dry film thickness (DFT) is one of the most important technical requirements for fire protective coatings. Manufacturers specify the required thickness according to the product formulation, substrate design and target fire-resistance period.
Procurement teams should verify:
Recommended wet film thickness.
Required dry film thickness.
Coverage rate per litre or kilogram.
Number of application coats.
Approved application methods.
Incorrect thickness can reduce the protective performance of the coating system.
Adhesion and Surface Compatibility
A coating must adhere properly to its substrate to provide reliable protection. Poor adhesion can cause peeling, cracking or detachment during normal operations or fire exposure.
Buyers should confirm compatibility with steel, concrete, wood or other specified surfaces. Surface preparation, primers and compatible topcoats also play an important role.
Moisture and Corrosion Resistance
Industrial facilities often expose coated surfaces to humidity, condensation, chemicals and outdoor weather conditions. These factors can damage protective coatings if the formulation does not provide suitable environmental resistance.
For steel structures, buyers should evaluate corrosion protection requirements alongside fire performance. A compatible primer and protective topcoat may be necessary to maintain the complete coating system.
Environmental and Application Requirements
Product selection should also consider VOC content, curing conditions, application temperature and workplace safety requirements. Water-based formulations may suit projects with stricter solvent-emission requirements, while other applications may require specialised solvent-based systems.
Manufacturers should provide technical data sheets, safety data sheets and application instructions to support safe handling and correct installation.
How Fire Retardant Coatings Are Applied and Tested
Proper application is essential because even a technically suitable product may fail to deliver its intended performance when contractors ignore preparation or installation requirements.
Surface Preparation and Application
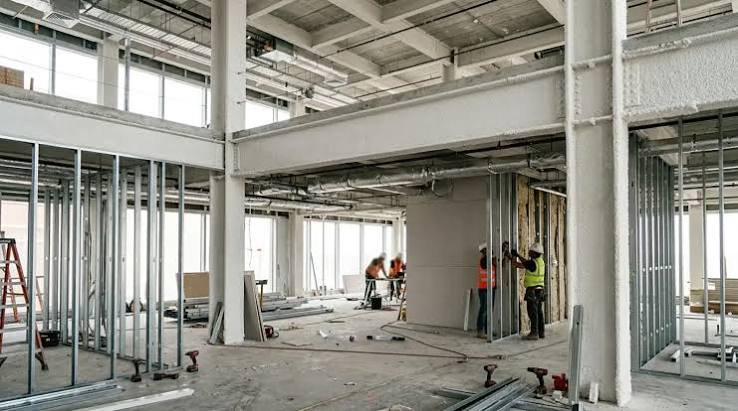
Before applying a fire retardant coating, contractors must prepare the substrate according to the manufacturer's instructions. Steel surfaces may require cleaning, removal of rust and application of an approved primer.
Application methods commonly include spraying, brushing and rolling, depending on the formulation and project requirements.
Testing and Quality Verification
Fire retardant coatings require appropriate testing to demonstrate their performance under defined conditions. Procurement teams should review recognised test standards and product-specific documentation.
Relevant standards and testing frameworks include:
ASTM E119: Evaluates the fire resistance of building construction and materials under specified test conditions.
UL 263: Covers fire tests of building construction and materials.
EN 13381 series: Addresses methods for determining the contribution of applied fire protection systems to structural elements.
These standards do not automatically apply to every coating or substrate. Buyers must confirm that the supplied product has been tested and approved for the intended application.
Quality inspections should also verify coating thickness, surface finish, adhesion and application consistency.
Procurement and Supply Chain Considerations
Sourcing fire retardant coatings requires coordination between technical teams, contractors, suppliers and procurement departments. A low-cost product may create additional expenses if it requires specialised application, frequent maintenance or replacement.
Evaluating Suppliers and Product Documentation
Before placing bulk orders, buyers should request:
Technical Data Sheets (TDS) with product specifications.
Safety Data Sheets (SDS) covering handling and storage.
Fire test reports from recognised laboratories.
Product certifications and approval documents where required.
Shelf-life and storage recommendations.
Application guidelines and compatibility information.
Suppliers should demonstrate that their products meet the project's technical requirements rather than relying on general marketing descriptions.
Storage, Transportation and Shelf Life
Fire retardant coatings require suitable storage conditions to maintain product quality. Extreme temperatures, direct sunlight and improper container handling can affect certain formulations.
Procurement teams should confirm packaging specifications, batch identification, manufacturing dates and remaining shelf life before accepting shipments. Water-based and solvent-based coatings may have different storage and transportation requirements.
Cost and Total Project Value
The purchase price represents only one part of the overall procurement cost. Buyers should also consider coverage rate, application labour, primer requirements, maintenance intervals and the expected service life of the coating system.
Comparing products through their technical performance and total installed cost helps procurement teams make better sourcing decisions.
Market Trends and Future Product Requirements
Industrial fire protection requirements continue to encourage demand for specialised coating technologies. Construction growth, infrastructure investment and industrial safety priorities create opportunities for manufacturers and chemical suppliers.
Several product development areas are gaining attention:
Lower-VOC formulations: Manufacturers are working on coatings that reduce solvent emissions while maintaining suitable performance.
Improved durability: Buyers increasingly value coatings that maintain adhesion and protection under demanding environmental conditions.
Advanced intumescent technology: Formulation development focuses on improving expansion behaviour, char stability and insulation performance.
Multifunctional coating systems: Some products combine fire protection with corrosion resistance to address multiple structural protection requirements.
Simplified application: Products with practical application requirements can help contractors improve installation efficiency and reduce project delays.
For chemical distributors and importers, these developments create opportunities to source specialised coating materials that meet changing construction and industrial requirements.
What Buyers Should Consider Before Sourcing
Selecting the right fire retardant coating requires a clear understanding of the project and its technical requirements. Buyers should avoid relying on a single specification or supplier claim when evaluating products.
The following considerations can help procurement teams improve purchasing decisions:
Identify the substrate: Confirm whether the coating will protect structural steel, concrete, wood or another material.
Define the fire protection target: Establish the required fire-resistance period and applicable testing standard.
Check application thickness: Verify the required DFT, coverage rate and number of coats.
Evaluate environmental exposure: Consider humidity, corrosion, chemical contact and outdoor conditions.
Verify product compatibility: Confirm that primers, topcoats and other system components work together.
Review supplier documentation: Request relevant test reports, certifications, TDS and SDS.
Compare total costs: Evaluate material consumption, application expenses and long-term maintenance requirements.
A technically approved product from a reliable supplier can help reduce project risks and support consistent fire protection across industrial facilities.
Antimony Trioxide (99.5%) - China
SOURCE LINK :https://store.astm.org/standards/e119
Found this useful?