Pulp and Paper Chemicals: Industrial Uses and Buyer Needs
Pulp and Paper Chemicals: Industrial Uses and Buyer Needs
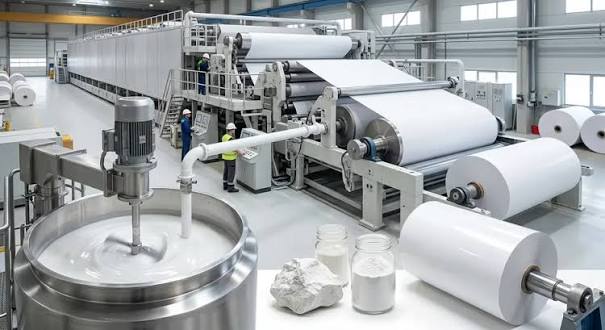
Pulp and paper chemicals are essential materials used to convert wood fibres and recycled paper into finished paper products. They support pulping, bleaching, de-inking, sheet formation, coating and wastewater treatment. These chemicals help manufacturers control fibre properties, improve paper strength, enhance brightness and maintain consistent production quality.
The pulp and paper industry manufactures a wide range of products, including printing paper, tissue, packaging board, corrugated materials and specialty papers. Each product requires a different combination of chemical additives based on its intended use and performance requirements.
For manufacturers and procurement teams, selecting the right chemicals involves evaluating technical specifications, production compatibility, supply reliability and environmental requirements. Understanding these factors helps mills improve efficiency while maintaining the quality of their finished products.
What Are Pulp and Paper Chemicals?
Pulp and paper chemicals are substances used during fibre processing and paper manufacturing to modify raw materials, control production conditions and improve finished-paper properties.
They generally fall into two major categories: process chemicals and functional chemicals.
Process Chemicals
Process chemicals improve manufacturing operations and support stable paper-machine performance. They help manage water removal, foam, deposits, microbial growth and fibre retention.
Common examples include:
Retention and drainage aids
Defoamers and deaerators
Biocides and slimicides
Dispersants and fixatives
De-inking chemicals
Deposit-control agents
Process-water treatment chemicals
These products help mills maintain production efficiency, reduce operational interruptions and improve process consistency.
Functional Chemicals
Functional chemicals directly influence the properties of the finished paper. Manufacturers use them to improve strength, brightness, colour, water resistance, printability and surface quality.
Common categories include sizing agents, dry-strength additives, wet-strength resins, mineral fillers, coating binders, dyes and optical brighteners.
The distinction between process and functional chemicals is not always absolute. Some additives influence both machine performance and final paper properties.
Chemicals Used in Pulping and Bleaching
Pulping is the first major stage of many paper manufacturing processes. It separates fibres from wood or other fibrous raw materials and prepares them for further processing.
Chemical requirements depend on the pulping method, raw material and desired pulp characteristics.
Pulping Chemicals
Chemical pulping uses reagents to separate cellulose fibres by removing or modifying lignin and other non-cellulosic components.
The kraft process is widely used in industrial pulp production. It relies primarily on sodium hydroxide and sodium sulphide in the cooking liquor to break down lignin and release fibres.
Other pulping systems use different chemical combinations. Sulphite pulping, for example, uses sulphurous acid and bisulphite chemistry under controlled conditions.
The selection of pulping chemicals depends on fibre quality requirements, wood species, recovery systems and mill operating conditions.
Bleaching Chemicals
Bleaching improves pulp brightness by removing or modifying residual lignin and coloured compounds. Manufacturers select bleaching sequences according to the pulp type, required brightness and environmental objectives.
Common bleaching chemicals include:
Hydrogen peroxide: Used in mechanical pulp bleaching and selected recycled-fibre applications.
Chlorine dioxide: An important bleaching agent in many modern chemical pulp bleaching sequences.
Oxygen: Used in oxygen delignification to reduce residual lignin before subsequent bleaching stages.
Ozone: Applied in selected bleaching processes to modify residual lignin and improve brightness.
Sodium hydrosulphite: Used as a reducing bleaching agent in selected mechanical pulp and recycled-paper applications.
Bleaching programmes require careful control of chemical concentration, temperature, pH and reaction time. Proper process management helps achieve the required brightness while protecting fibre quality.
Coating Binders and Additives
Coating formulations are applied to paper surfaces to improve smoothness, brightness, printability and appearance.
Common coating ingredients include mineral pigments, starch and polymer binders. Styrene-butadiene latex and other synthetic binders help hold coating particles together and improve coating integrity.
Rheology modifiers, dispersants and lubricants may also be added to control coating viscosity, stability and application behaviour.
The coating formulation must match the paper grade, coating equipment, drying conditions and final printing requirements.
Dyes and Optical Brightening Agents
Dyes provide specific colours, while optical brightening agents improve the apparent whiteness of paper by absorbing ultraviolet light and emitting blue light.
These additives are used in selected printing, writing and specialty paper grades. Their performance depends on compatibility with the pulp, coating system and other formulation ingredients.
Water Treatment and Process-Control Chemicals
Pulp and paper mills use large quantities of water throughout manufacturing. Process-water quality affects chemical performance, machine cleanliness and product consistency.
Water treatment chemicals help control suspended solids, dissolved contaminants, microorganisms and wastewater characteristics.
Coagulants, Flocculants and Defoamers
Coagulants destabilise suspended particles, while flocculants encourage small particles to form larger aggregates that can be separated more easily.
Polyacrylamide-based flocculants and aluminium-based coagulants are used in selected clarification and wastewater treatment systems.
Defoamers reduce unwanted foam in pulp preparation, washing, bleaching and paper-machine operations. Excessive foam can interfere with equipment performance, drainage and production stability.
Biocides and Deposit-Control Chemicals
Warm, water-rich paper manufacturing systems can encourage microbial growth. Biocides and slimicides help control unwanted biological activity and reduce slime formation.
Deposit-control chemicals also help manage pitch, adhesives and other contaminants that accumulate on machine surfaces.
The correct treatment programme depends on water circulation, temperature, microbial conditions and the nature of the contaminants.
Key Buyer Needs When Sourcing Pulp and Paper Chemicals
Selecting the right chemical supplier is important for mills that require consistent product performance and uninterrupted production. Buyers should evaluate more than the quoted price and consider the chemical's suitability for their specific manufacturing process.
Technical Specifications and Product Compatibility
Procurement teams should request a current technical data sheet and safety data sheet before purchasing. Depending on the chemical, important parameters may include:
Chemical composition and active content
Purity and concentration
pH, viscosity and density
Solubility and dispersion properties
Molecular weight and charge density for polymer products
Particle size and brightness for mineral fillers
Moisture content and storage stability
Recommended dosage and application conditions
Compatibility with existing additives is also important. A chemical that performs well independently may interact differently when combined with other products in a mill's system.
Consistent Quality and Reliable Supply
Paper manufacturing often operates continuously, making consistent chemical availability essential. Variations in product quality can affect production conditions, finished-paper properties and chemical consumption.
Buyers should assess suppliers based on batch consistency, quality-control procedures, documentation, packaging and delivery reliability.
A certificate of analysis can help verify that each supplied batch meets the agreed specifications.
Cost, Performance and Sustainability
The most economical chemical is not necessarily the product with the lowest purchase price. Mills should consider dosage requirements, production performance, equipment maintenance, waste generation and the impact on finished-product quality.
Environmental considerations also influence purchasing decisions. Buyers increasingly evaluate chemical efficiency, wastewater compatibility, biodegradability where relevant and compliance with applicable regulations.
For paper products intended for food-contact applications, mills should also verify relevant regulatory requirements and supplier documentation for the intended use.
Safe Handling and Storage Requirements
Pulp and paper chemicals have different hazard profiles. Acids, alkalis, oxidising agents, biocides, polymers and solvents each require appropriate handling procedures.
Facilities should follow the product-specific safety data sheet and site chemical-management programme. Suitable controls may include protective gloves, eye protection, ventilation, dust control and designated chemical transfer equipment.
Store products in compatible, clearly labelled containers under recommended temperature and moisture conditions. Keep incompatible substances separated and maintain appropriate spill-response procedures.
Pulp and paper chemicals support nearly every stage of paper manufacturing, from fibre preparation and bleaching to sheet formation, coating and wastewater treatment. Selecting suitable products requires careful attention to technical specifications, process compatibility, consistent supply and environmental responsibilities.
A reliable sourcing strategy helps paper manufacturers maintain product quality, improve operational efficiency and respond to changing customer and industry requirements.
Calcium Carbonate (Feed Grade)
Found this useful?