Scale Inhibitors: Applications in Water Systems and Industrial Operations
Mineral scale remains one of the most persistent challenges in industrial water management, affecting equipment performance, energy consumption and maintenance costs. Scale inhibitors help industrial operators control mineral precipitation before it develops into hard deposits that restrict water flow and damage equipment.
Industries that depend on continuous water circulation face particular challenges because evaporation, temperature changes and mineral concentration increase the likelihood of scale formation. Cooling towers, boilers, desalination facilities, power plants and oil and gas operations all rely on effective scale management to maintain consistent performance.
As industrial facilities place greater emphasis on operational efficiency and water conservation, scale inhibitors have become an important part of modern water treatment strategies. Their ability to control mineral deposits supports longer equipment life, more reliable production and better resource utilization.
Understanding Scale Inhibitors and Their Chemical Function
Scale inhibitors are specialty chemicals that prevent or reduce the formation of mineral deposits on surfaces exposed to water. These deposits commonly contain calcium carbonate, calcium sulfate, magnesium salts, silica and other poorly soluble compounds.
Scale develops when dissolved minerals exceed their solubility limits under particular operating conditions. Changes in temperature, pressure, pH and dissolved mineral concentration can encourage these substances to separate from water and accumulate on pipes, membranes, heat exchangers and other equipment.
Scale inhibitors work through several chemical mechanisms:
Threshold inhibition: These chemicals delay the formation and growth of mineral crystals, allowing water to retain higher concentrations of dissolved minerals without immediate precipitation.
Crystal modification: Certain additives interfere with crystal development and produce deposits with structures that attach less readily to equipment surfaces.
Dispersion: Polymeric compounds help keep fine mineral particles suspended in water, reducing their tendency to accumulate and form dense deposits.
Sequestration: Chelating agents bind selected metal ions and reduce their availability for forming insoluble compounds.
Common scale control formulations include phosphonates, polyacrylates, polymaleates and other specialized polymeric compounds. Treatment providers select formulations according to water chemistry, operating temperature and the specific minerals responsible for scaling.
Major Applications Across Industrial Water Systems
Scale inhibitors support several industrial processes where mineral deposits can interfere with equipment performance. Each application presents different water chemistry conditions and operating requirements.
1. Cooling Towers and Industrial Cooling Systems
Cooling towers represent one of the largest application areas for scale inhibitors. Water evaporates during the cooling process, leaving dissolved minerals behind and increasing their concentration in the circulating water.
Without proper treatment, calcium carbonate and calcium sulfate deposits can accumulate on cooling tower fill, condenser tubes and heat exchange surfaces. These deposits reduce heat transfer efficiency and restrict water circulation.
Scale inhibitors help maintain mineral stability and allow facilities to operate at higher cycles of concentration when water chemistry permits. This can reduce freshwater consumption and limit the volume of water discharged through blowdown.
2. Boiler Systems and Steam Generation
Boilers operate under elevated temperatures and pressures, creating conditions where dissolved minerals can precipitate rapidly. Scale formation on heating surfaces reduces heat transfer and increases fuel consumption.
Industrial water treatment programs use appropriate scale-control chemicals alongside feedwater pretreatment and other conditioning methods. Operators must also monitor water hardness, alkalinity and conductivity to prevent unwanted mineral accumulation.
3. Reverse Osmosis and Desalination Plants
Reverse osmosis systems face significant scaling risks because membranes concentrate dissolved minerals as water passes through the treatment process. Calcium carbonate, calcium sulfate, silica and other compounds can accumulate on membrane surfaces.
Specialized antiscalants help maintain membrane performance by delaying mineral precipitation. Their application supports stable water production, reduces cleaning frequency and helps protect expensive membrane components.
4. Oil and Gas Production
Oil and gas operations encounter scaling problems when changes in pressure, temperature and water composition cause dissolved minerals to precipitate. Calcium carbonate, barium sulfate, strontium sulfate and calcium sulfate can create deposits in production tubing, pipelines and processing equipment.
Specialized scale inhibitors help control these deposits during extraction, transportation and processing. Depending on the reservoir and operating conditions, operators may inject treatment chemicals continuously or use controlled treatment programs to maintain protection.
Key Industries Driving Scale Inhibitor Demand
Demand for scale inhibitors extends beyond conventional water treatment. Industrial expansion, infrastructure investment and increasing water reuse requirements create opportunities across several sectors.
The most important consuming industries include:
Power generation: Thermal power plants use extensive cooling and boiler systems that require consistent scale management to maintain heat transfer efficiency and equipment reliability.
Chemical manufacturing: Processing facilities depend on heat exchangers, cooling circuits and water treatment systems where mineral deposits can interrupt production.
Petrochemicals and refining: Refineries use treated water across cooling, steam generation and processing operations, creating demand for specialized deposit-control chemicals.
Municipal water treatment: Drinking water facilities and wastewater treatment plants use suitable chemical treatment programs to manage mineral deposits in pipes and processing equipment.
Food and beverage manufacturing: Production facilities require reliable water systems for processing, cleaning and temperature control, making deposit prevention an important maintenance consideration.
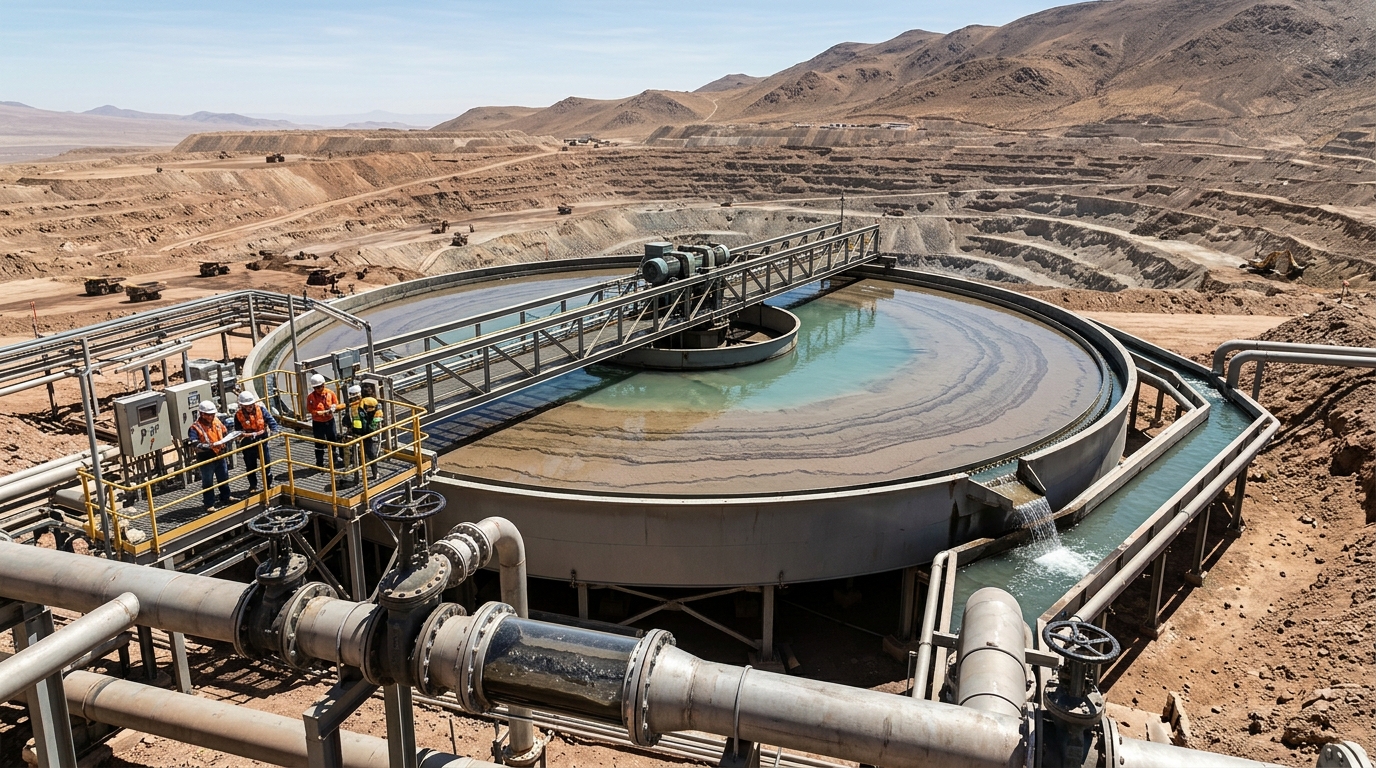
Mining and mineral processing: Water-intensive operations face scaling challenges in pipelines, evaporation systems and mineral recovery processes.
Growing industrial activity in developing economies also creates opportunities for chemical suppliers. Expanding manufacturing capacity and investment in water infrastructure increase the need for dependable water treatment chemicals.
Factors That Influence Scale Inhibitor Selection
Selecting an appropriate scale inhibitor requires more than identifying the mineral responsible for deposits. Procurement teams and industrial operators must evaluate the complete water treatment environment before approving a chemical formulation.
Several technical factors influence product selection:
Water composition: Calcium, magnesium, sulfate, bicarbonate, silica and other dissolved substances determine the type of scale that may develop. Water analysis helps identify the minerals that require treatment.
Operating temperature and pressure: High temperatures can change mineral solubility and increase precipitation risks. Oilfield operations and industrial boilers often require formulations designed for demanding temperature and pressure conditions.
pH and alkalinity: These parameters influence mineral solubility and chemical compatibility. Calcium carbonate scaling, for example, becomes more likely under certain high-pH and high-alkalinity conditions.
System design: Flow velocity, residence time, equipment materials and circulation patterns affect how deposits develop and where they accumulate.
Chemical compatibility: Scale inhibitors must work effectively alongside corrosion inhibitors, biocides and other water treatment chemicals. Incompatible formulations can reduce treatment performance or create additional operating problems.
Environmental requirements: Discharge restrictions and local chemical regulations influence the choice of treatment ingredients, particularly in facilities that release treated water into regulated environments.
A reliable treatment program combines laboratory water analysis, appropriate chemical selection and regular monitoring. Incorrect dosage or unsuitable formulations can leave equipment exposed to scaling even when operators use treatment chemicals consistently.
Supply Chain and Procurement Considerations
The industrial scale inhibitor market depends on a specialized supply chain involving chemical manufacturers, formulation companies, distributors and water treatment service providers. Raw material availability, manufacturing capacity and international freight conditions can influence purchasing costs and delivery schedules.
Many commercial formulations use phosphonates and polymer-based ingredients. Their production depends on access to chemical intermediates, consistent manufacturing processes and suitable quality control systems.
For international buyers, several sourcing considerations deserve attention:
Supplier reliability: Evaluate manufacturers and distributors based on their experience, product consistency and ability to maintain regular supply.
Technical documentation: Request Safety Data Sheets (SDS), Technical Data Sheets (TDS) and relevant product specifications before placing orders.
Product concentration: Compare active ingredient content rather than relying exclusively on the quoted price per kilogram or litre.
Packaging and transportation: Confirm packaging compatibility, storage conditions and transport requirements, particularly for bulk chemical shipments.
Lead times: Account for manufacturing schedules, export documentation, shipping arrangements and customs clearance when planning procurement.
Quality consistency: Request certificates of analysis and confirm that delivered material meets the agreed specifications.
Buyers should also distinguish between concentrated active ingredients and ready-to-use formulations. Their pricing, handling requirements and application costs can differ considerably.
Sustainability and Water Conservation in Scale Control
Water conservation has become an important consideration for industries operating large cooling systems and water-intensive production facilities. Scale inhibitors contribute to this objective by helping treatment systems maintain performance while managing higher concentrations of dissolved minerals.
In cooling towers, effective chemical treatment can support higher cycles of concentration. This reduces the amount of freshwater required for makeup water and can lower blowdown volumes, depending on the system's operating limits and water chemistry.
Scale control also supports energy efficiency. Mineral deposits act as insulating layers on heat transfer surfaces, forcing equipment to consume more energy to achieve the same thermal performance.
Several developments are influencing the sustainability direction of the industry:
Phosphorus-free formulations: Some manufacturers are developing alternative treatment chemistries to address concerns about phosphorus discharge into aquatic environments.
Advanced polymer technology: Specialized polymers offer opportunities to improve deposit control under challenging water conditions.
Water reuse: Industrial facilities increasingly incorporate reclaimed water into their operations, creating demand for treatment programs that can manage variable mineral concentrations.
Automated chemical dosing: Monitoring systems and controlled dosing equipment help maintain treatment levels while reducing unnecessary chemical consumption.
Integrated treatment programs: Combining filtration, pretreatment and chemical inhibition can improve overall water management and reduce avoidable waste.
Sustainable scale management requires balancing chemical effectiveness, water consumption, energy efficiency and environmental discharge requirements. The most suitable approach depends on the individual facility and its operating conditions.
Market Outlook and Opportunities for Chemical Buyers
Industrial demand for scale inhibitors will continue to benefit from investment in water treatment infrastructure, manufacturing facilities and energy production. Growing attention to water reuse and operational efficiency also creates opportunities for suppliers offering specialized treatment chemicals.
Reverse osmosis installations represent an important area of demand because membrane systems require effective antiscalant programs to maintain performance. Expansion in desalination and industrial wastewater recycling further strengthens the importance of mineral deposit control.
Oil and gas operations also require advanced solutions for controlling carbonate and sulfate deposits under challenging production conditions. Meanwhile, power generation and chemical manufacturing continue to depend on reliable cooling and boiler water treatment programs.
For chemical traders and procurement managers, several opportunities stand out:
Specialty chemical distribution: Build relationships with manufacturers offering phosphonate-based and polymer-based scale control ingredients.
Regional industrial supply: Target manufacturing hubs, power plants and water treatment contractors with recurring chemical requirements.
Technical product differentiation: Prioritize suppliers that provide application-specific formulations and consistent technical documentation.
Sustainable product portfolios: Evaluate alternatives designed for lower environmental impact and compatibility with water reuse systems.
Long-term procurement agreements: Establish dependable supply arrangements to reduce the risk of treatment interruptions and unexpected purchasing costs.
Buyers should focus on total treatment economics rather than the initial chemical purchase price. A formulation that provides reliable scale control at an appropriate dosage can deliver greater value through reduced maintenance, lower energy consumption and improved equipment availability.
What Industrial Buyers Should Prioritize When Sourcing Scale Inhibitors
Effective scale management depends on selecting chemicals that match the water composition and operating requirements of each industrial system. A product that performs well in a cooling tower may not provide the same results in a reverse osmosis plant or oilfield production system.
Procurement teams should prioritize verified suppliers, consistent product specifications and reliable technical support. Comparing active content, treatment requirements, compatibility and delivery reliability can help buyers make better purchasing decisions.
As industrial facilities invest in water conservation and more efficient operations, the need for dependable scale control solutions will remain significant. Chemical suppliers that combine consistent quality with competitive pricing and responsive logistics can serve this demand across multiple industrial sectors.
Ready to source Sodium Gluconate from verified global suppliers? Explore competitive offers on our platform today.
Sources:
Monosodium Glutamate (E621)
Found this useful?